Expert insight
Airnord: Continuing the FLSmidth Airtech story in emissions control – with an even sharper focus on the cement industry
Expert insight
Airnord: Continuing the FLSmidth Airtech story in emissions control – with an even sharper focus on the cement industry
Airnord is the new home of FLSmidth’s former Air Pollution Control business. In this article, Airnord specialists explain how decades of experience with electrostatic precipitators, gas cleaning and cement applications continue under the Airnord name – with an increased focus on emissions performance, plant productivity and carbon capture integration.
Airnord is the new home of FLSmidth’s Air Pollution Control (APC) business. And while the name has changed, the expertise gained from thousands of ESP and other APC installations has not.
That continuity couldn’t come at a better moment for cement producers. Because despite undergoing rapid changes, the industry still faces numerous emissions hurdles.
Cement industry changes create new emissions challenges
For Linda Ravn Nyhauge, Sales Manager at Airnord, changing fuels or adopting a decarbonisation strategy create their own challenges: ‘Plants still have to minimise emissions of sulfur dioxide (SO₂) and hydrogen chloride (HCl).’
The good news is that Airnord’s APC expertise helps producers overcome these issues.
‘We’re known for electrostatic precipitators,’ says Nyhauge. ‘For a plant that already has one installed, that could mean a new cooler filter or a retrofit of the existing ESP. But we are also strong in lowering gas emissions.’
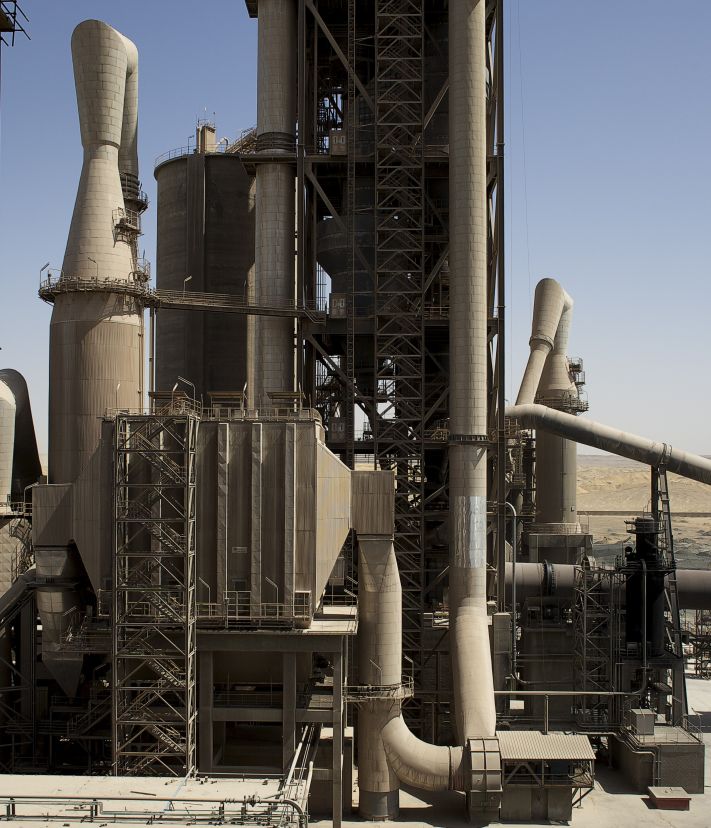
Our proprietary Gas Suspension Absorber technology, for example, is highly efficient at removing SO₂. Put simply, lime slurry reacts with process gases, converting them into solids that can be removed.
GSA desulphurisation: making lime work over and over again
For Nyhauge’s colleague Jesper Anders Lund, Sales & Project Manager at Airnord, the really clever part of GSA comes next.
‘Instead of using the absorbent once, the GSA recirculates the partially reacted material, effectively giving the lime another chance – up to 100 of them – to do its job.’
This recirculation helps achieve high removal efficiency. And as the process is semi-dry, it avoids the large liquid effluent stream associated with conventional wet scrubbing.
GSA’s flexibility extends to how it’s deployed. Lund explains: ‘It can be an add-in to an existing plant, working with whatever dust filter is already installed, whether that’s a fabric filter or an ESP. Or it can form part of a new installation, including flue gas cooling, the GSA itself and a new ESP or fabric filter.’
Whatever the deployment, the underlying chemistry stays the same: a semi-dry process in which reaction by-products are reused, delivering high lime efficiency at low stoichiometry – and SO₂ removal above 97%.
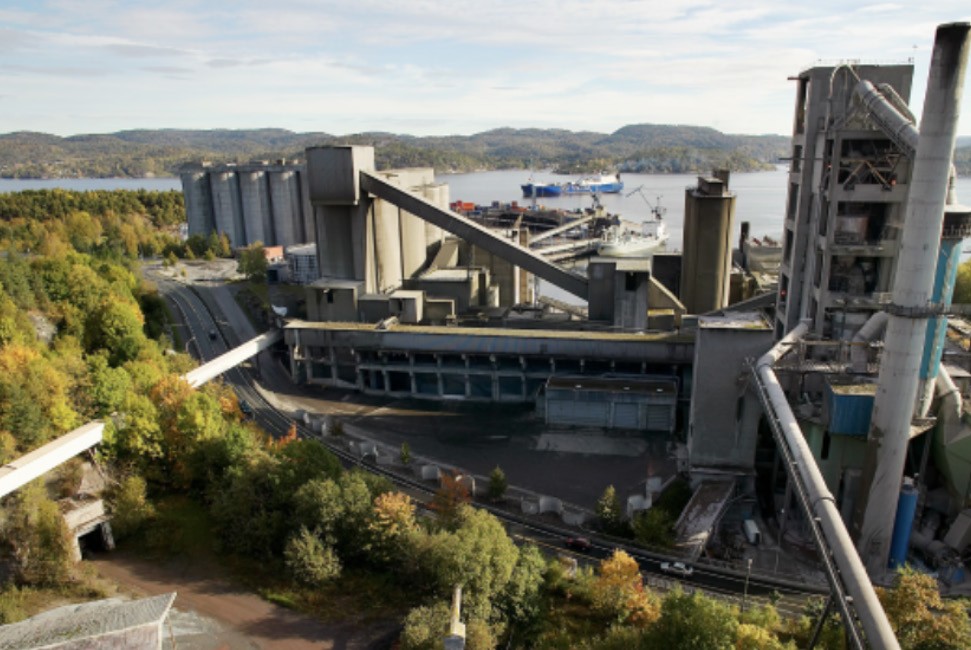
‘GSA is our technology,’ says Nyhauge. ‘We have GSA systems running worldwide, including at what used to be the Norcem – now Heidelberg Materials – cement plant in Norway.’
Brevik GSA cuts SO₂ from 405 to 10.8 mg/Nm³
The case mentioned by Lund involved the plant cutting annual SO₂ emissions by around 400 tonnes.
Its challenge was complicated by the raw materials used: one raw mix generated negligible SO₂, another could produce concentrations of up to 400 mg/Nm³. The plant therefore wanted technology that could be used for the higher-emitting mix.
The solution was a GSA system that lowered SO₂ concentrations from 405 mg/Nm³ to 10.8 mg/Nm³ at the outlet – a reduction of 97.3%.
HCl emissions fell 95.2%, from 34 to 1.6 mg/Nm³.
High removal efficiency in a compact footprint
The Brevik case demonstrates another consideration familiar to practically every cement plant: there isn’t much spare room.
Yet the GSA unit slotted into a footprint of around only 50 square metres.
Supporting carbon capture integration at Heidelberg Materials Brevik
Airnord’s expertise in APC for cement is now being brought to bear on another important area: carbon capture.
Long the subject of decarbonisation plans, capture units are now being deployed at cement plants.
One landmark was the 2025 opening of the Heidelberg Materials Carbon Capture and Storage (CCS) unit at the Brevik plant.
‘The plant’s former owner started talking about CCS in 2005,’ says Lund, ‘and we have been involved for a good part of the journey.’
Indeed, according to Anders Skærlund Petersen, Senior Project Manager, Brevik CCS at Heidelberg Materials, such commitment is an Airnord strength:
“Airnord kept the same team from FEED to startup, evaluating and upgrading critical APC equipment. Their input was invaluable to integrating the CCS unit.”
– Anders Skærlund Petersen
Senior Project Manager, Brevik CCS at Heidelberg Materials
A cement industry in flux needs proven APC expertise
With recent heatwaves putting decarbonisation at the centre of policy debates, there will no doubt be renewed pressure for the cement industry to accelerate its adoption of CCS.
Paradoxically, it will be proven partners such as Airnord who will help plants navigate the challenges ahead.
‘Whether it’s a retrofit, a new installation, or a pre-FEED or FEED study for carbon capture, we thrive on being involved all the way to execution,’ adds Nyhauge.
After all, as Petersen puts it:
‘Airnord’s heritage brings immense knowledge and flexibility to today’s complex APC upgrades for cement plants.’